A factory tour shows capacity; an audit tests whether the supplier can repeatedly build the approved product. For industrial LED lighting, focus on design control, component traceability, process controls, electrical safety tests and change management.
Audit objective: follow one finished luminaire backward from carton to critical components and forward from incoming inspection to final test. If the records cannot connect those steps, traceability is incomplete.
Prepare a product-specific audit plan
Send the exact SKU, drawings, critical-to-quality characteristics and target-market requirements before the visit. Ask the factory to make the proposed product during the audit if practical. A line producing an unrelated downlight does not demonstrate control of a 600 W floodlight.
Review the LM-79, LM-80 and TM-21 evidence guide first so the audit can connect documents to the actual bill of materials.
1. Verify design and document control
Check drawing approvals, revision history, engineering change notices and access permissions. Select a current work instruction on the line and compare it with the master revision. Ask how obsolete files and jigs are removed from use.
Look for controlled specifications covering torque, thermal interface material, gasket compression, wiring, driver programming, surge protection and photometric configuration.
2. Trace critical incoming components
Sample LED packages, drivers, SPDs, lenses, gaskets, cable glands and fasteners. Review supplier approval, incoming criteria, lot identification and storage conditions. For moisture-sensitive LEDs, check handling and bake controls where applicable.
Ask the auditor to choose the sample. A pre-arranged “show lot” provides little confidence.
3. Observe production controls
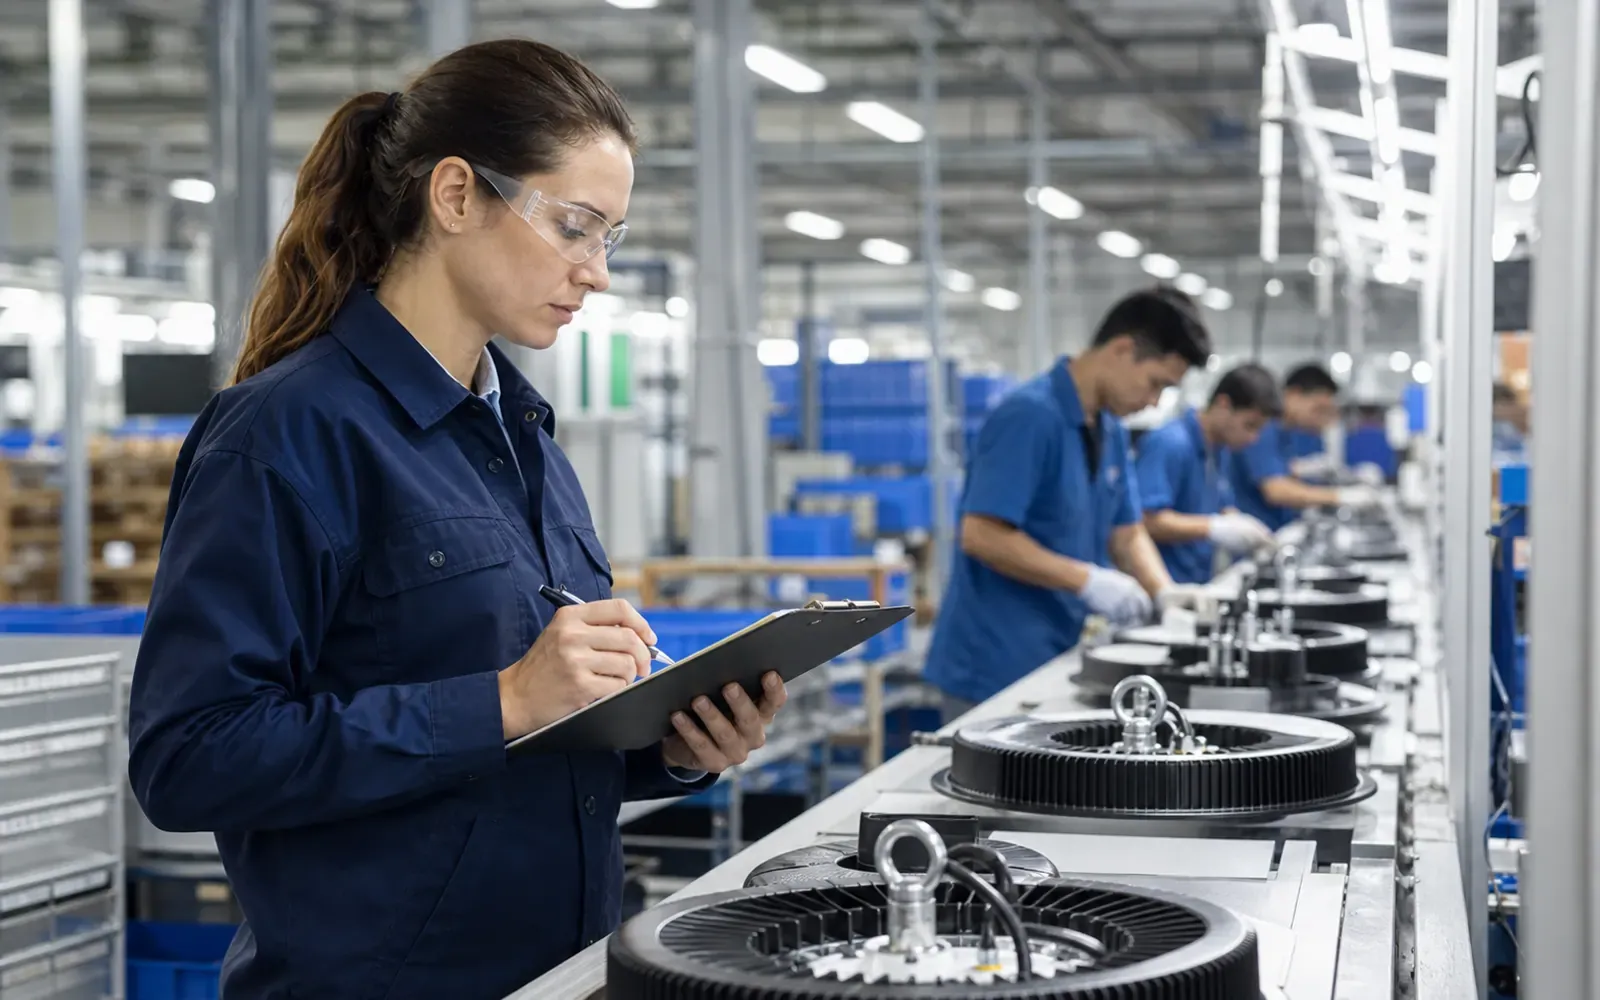
Walk the actual process and record how operators verify:
- heat-sink and PCB cleanliness;
- thermal material amount and coverage;
- screw torque and sequence;
- earth bonding;
- gasket placement and cable-gland tightening;
- driver programming;
- lens/optic identity;
- label and carton code.
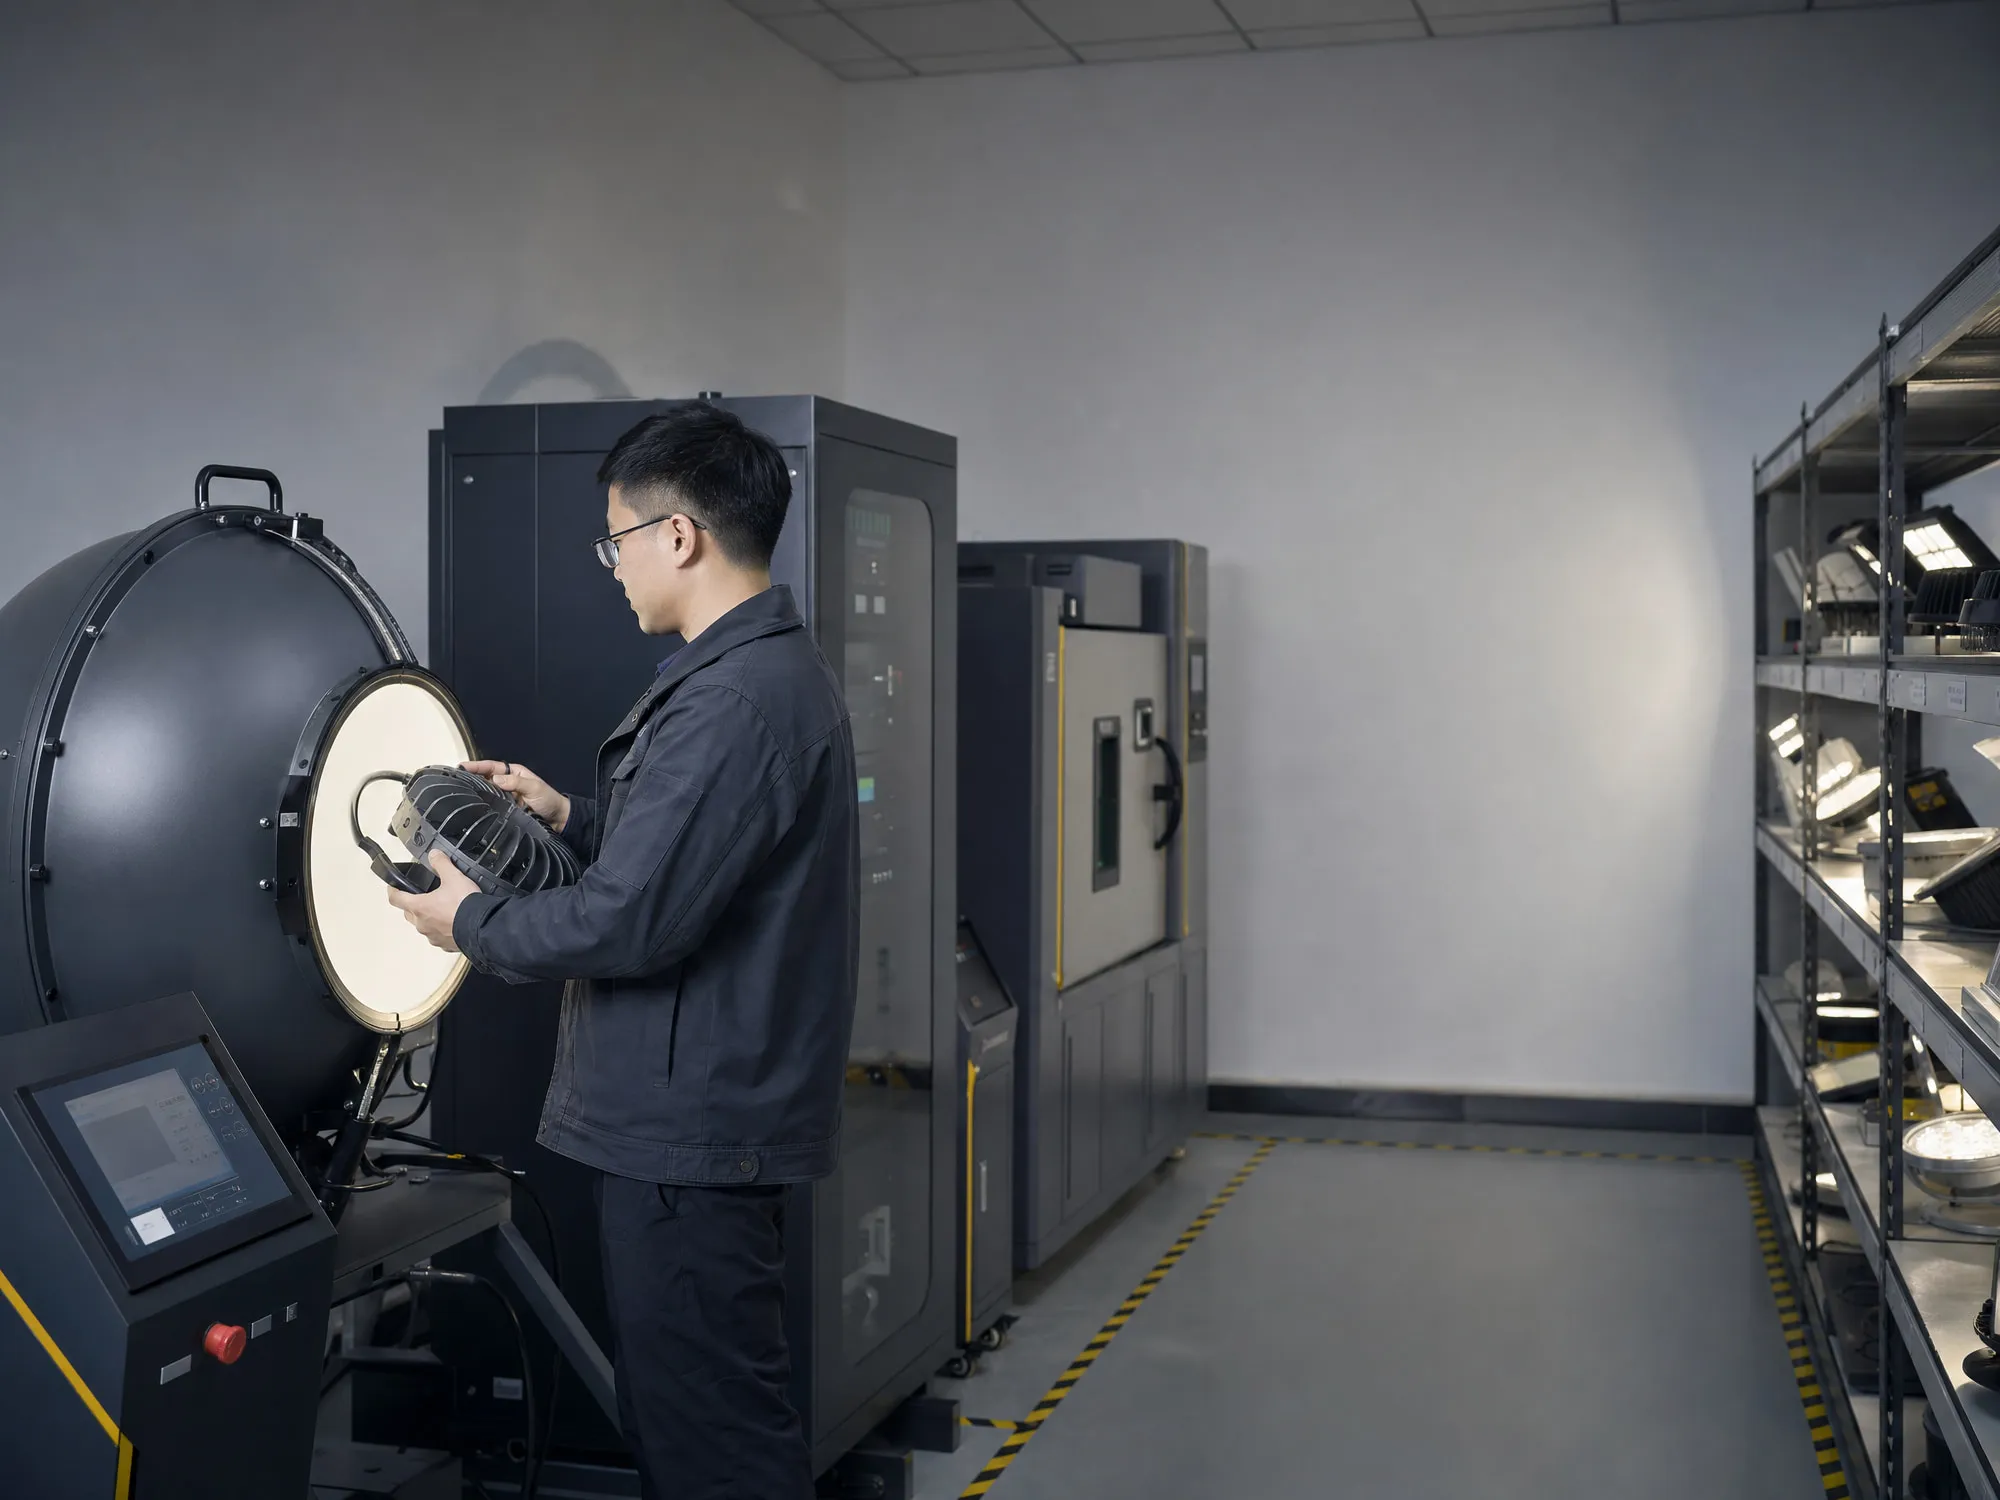
Calibrated tools should have a visible status and a record traceable to recognized standards. Review what happens when a tool is found out of calibration.
4. Review in-process and final testing
Define which tests run on every unit and which are sampled. Depending on the product and certification scheme, production checks may include earth continuity, dielectric strength, insulation, functional power, dimming, burn-in and visual inspection.
UL explains that complete luminaires and recognized internal components have different certification roles (UL lighting standards and certification). Confirm that the factory’s routine tests match the conditions required for the product’s target-market certification.
5. Test nonconformance and corrective action
Choose a recent defect and follow it through quarantine, investigation, rework approval, retest and disposition. Look for root-cause analysis based on evidence rather than “operator error” as a default conclusion.
Check whether reworked units are visibly identified and whether repeated failures trigger escalation. Review customer-return data by failure mode and production lot.
6. Challenge change management
Ask what happens if the approved driver becomes unavailable. A robust process requires technical review, validation, document updates and buyer approval where contracted. Critical substitutions should not be treated as purchasing decisions alone.
Your purchase agreement should list controlled components and notification periods. Keep an approved golden sample and signed specification for comparison.
7. Confirm packaging and shipment controls
Industrial luminaires are heavy and may travel through humid ports. Review carton strength, internal supports, moisture protection, pallet pattern and drop/vibration validation. Confirm that product and carton labels preserve lot traceability after installation.
Score evidence, not presentation
Use a simple severity scale:
- Critical: safety, certification or systemic traceability failure;
- Major: process can produce nonconforming product without detection;
- Minor: isolated control gap with low immediate risk;
- Observation: improvement opportunity.
Set owners and due dates. Require objective closure evidence, such as revised instructions, training records, photos, test results or a follow-up sample.
Audit deliverables
The final record should include scope, products observed, production status, evidence sampled, findings, photographs where permitted, corrective-action deadlines and residual risks. Protect confidential factory information and follow agreed access rules.
Combine this audit with a pilot order and pre-shipment inspection. The industrial lighting RFQ checklist covers project inputs, while this audit evaluates whether the chosen supplier can hold the specification across production.