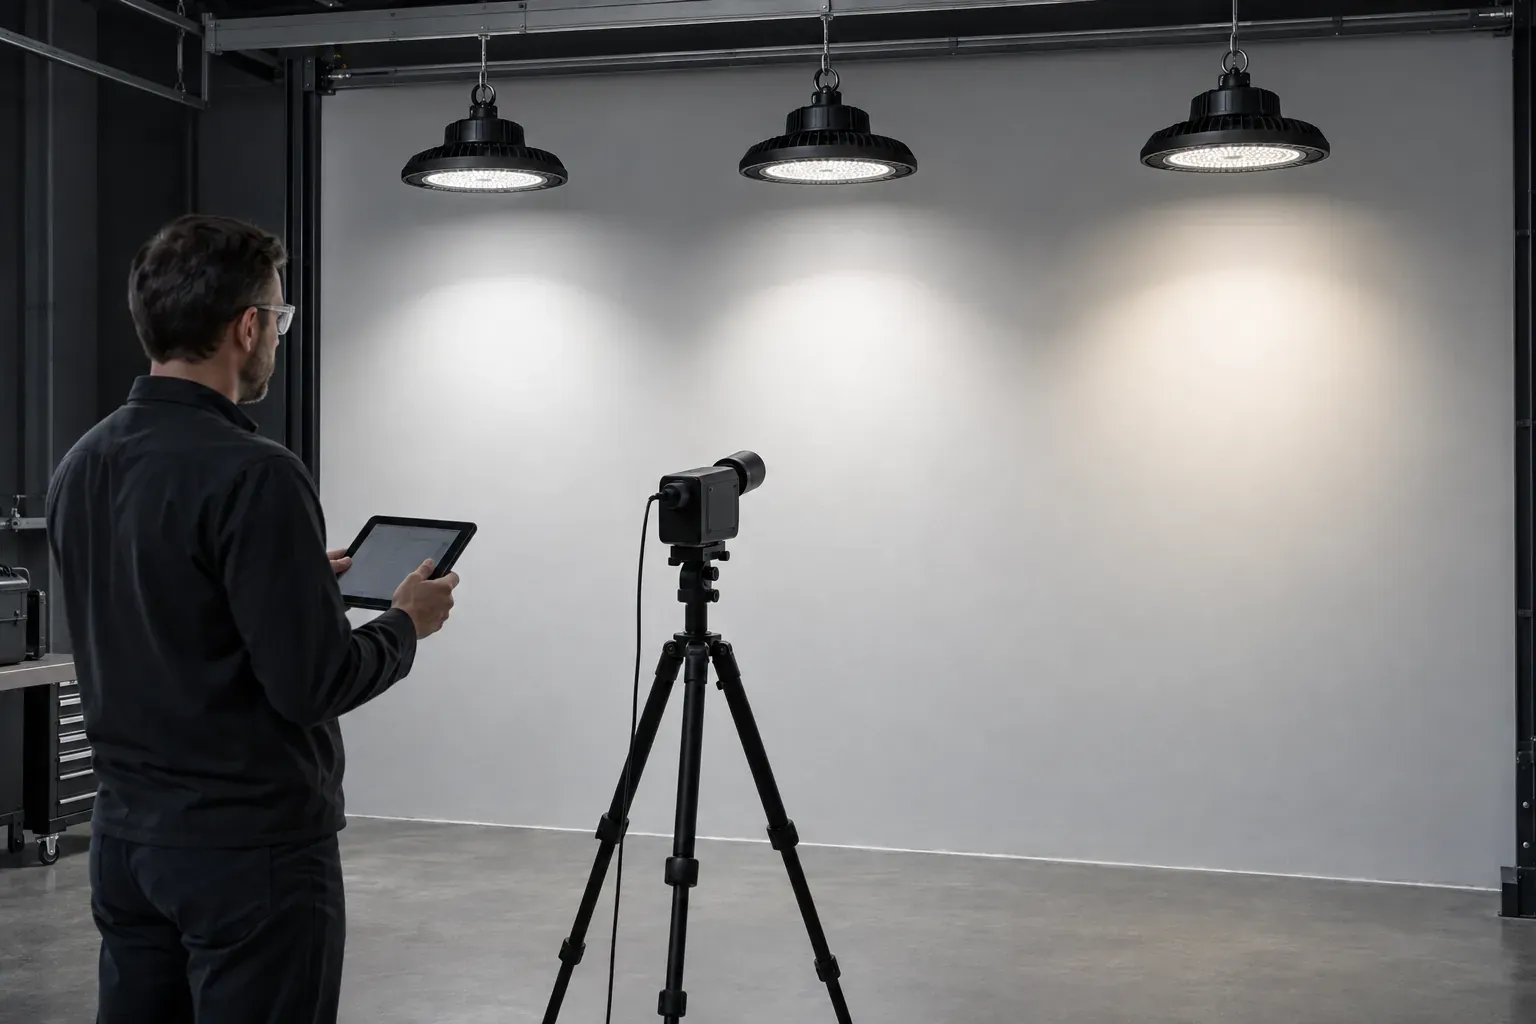
Two LED high bays can both be labeled 4000K yet produce visibly different white light. One may look slightly green, pink, warm or cool beside the other. Correlated color temperature identifies a broad white-light appearance; it does not by itself control the chromaticity spread between luminaires.
For B2B buyers, 3 SDCM vs 5 SDCM LED high bay is therefore a production-consistency decision, not a decorative datasheet detail. The correct requirement depends on sightlines, illuminated surfaces, batch size, replacement strategy and the cost of correcting a mismatched installation.
Short answer: should an industrial project specify 3 SDCM or 5 SDCM?
Specify 3 SDCM or tighter when multiple luminaires or their light patterns are seen together, when they illuminate white or neutral surfaces, when visual inspection is important, or when color mismatch would trigger expensive access and replacement work. Consider 5 SDCM for cost-sensitive general industrial zones where fixtures are widely separated, surfaces are visually complex and small tint differences are unlikely to affect the task.
Do not approve either number without defining the target chromaticity, measurement conditions, sample plan and whether the limit applies to the complete luminaire. A 3-SDCM LED package does not automatically make the assembled high bay a verified 3-SDCM product.
1. What SDCM and MacAdam steps describe
SDCM means standard deviation of color matching. In common lighting specifications, “3-step MacAdam” and “3 SDCM” describe a chromaticity-tolerance region around a stated center point. A lower step count means a tighter allowed region.
However, the number should not be interpreted as a simple percentage of visible difference. CIE TN 001:2014 explains that chromaticity differences are needed for several distinct issues—including product-to-product variation, angular uniformity and change during life—and that MacAdam ellipses vary in size and shape across chromaticity space. “Five steps” is not a universal promise that every observer, surface and installation will react in the same way.
For procurement, use SDCM as a tolerance boundary that can be measured and audited. Do not turn it into an unsupported statement such as “3 SDCM is invisible to everyone.”
2. SDCM is not the same as CCT, CRI or color maintenance
These parameters answer different questions:
| Parameter | Main question | What it does not prove |
|---|---|---|
| CCT | Does the light appear broadly warm, neutral or cool? | That all 4000K luminaires match one another |
| Initial SDCM | How tightly are initial chromaticities grouped around a target? | That color remains stable through life |
| CRI or TM-30 | How does the source render object colors? | That two luminaires have the same white point |
| Color maintenance | How much does chromaticity change after operation? | That the initial batch was tightly matched |
| Angular color uniformity | Does color change across viewing or beam angles? | That separate luminaires match each other |
Use the 4000K vs 5000K high-bay guide to choose the nominal CCT. Use the TM-30 vs CRI guide when the task involves judging materials, finishes or product colors. Then specify initial color consistency separately.
3. Choose the tolerance from the visual risk
Do not apply one step count to an entire site without reviewing where differences will be visible.
| Project zone | Color-mismatch risk | Practical starting point |
|---|---|---|
| High open warehouse with mixed stock and wide spacing | Low to moderate | 5 SDCM may be proportionate if verified |
| Long rack aisle with repeated fixtures | Moderate; rows make differences easier to compare | 3 SDCM is safer |
| White ceiling, wall-wash or clean production room | High; neutral surfaces expose tint differences | 3 SDCM or tighter |
| Quality-control or color-inspection station | High and task-related | Define SDCM plus CCT, Duv and color-rendering needs |
| Loading yard with isolated poles | Usually lower | 5 SDCM may be acceptable, subject to client expectations |
| Phased project or frequent replacements | High cross-batch risk | Tight initial limit plus bin and spare-stock plan |
Also consider access cost. A slightly mismatched unit at 12 meters may require a lift, shutdown and safety permit to replace. The visual tolerance should reflect the consequence of failure, not just what the LED supplier can offer most cheaply.
4. Define the center point, not only the ellipse size
An SDCM value needs a center. Two suppliers can each claim 3 SDCM while using different target chromaticity coordinates within the same nominal CCT region. Their products may therefore look different when mixed.
Ask the supplier to declare:
- nominal CCT and target chromaticity coordinates;
- coordinate system and calculation method used;
- maximum SDCM steps around that target;
- whether a Duv target or range is controlled;
- rated input, dimming level, ambient condition and stabilization method;
- measurement uncertainty and the rule used at the tolerance boundary.
The European Commission’s official ecodesign FAQ illustrates the principle: suppliers declare chromaticity coordinates and MacAdam steps, and verification examines whether measured products remain within the declared boundary. Even when a regulation is not the contract basis, the same discipline makes a B2B specification auditable.
5. Verify the complete luminaire at operating conditions
IEC 62722-2-1:2023 specifies performance requirements, test methods and conditions for LED luminaires. IEC 62717 addresses LED-module performance. This distinction matters: module evidence supports component selection, while the buyer receives a complete luminaire with a driver, thermal path, optics and control settings.
Chromaticity can be influenced by LED bin selection, junction temperature, drive current, optical materials and phosphor or lens behavior. Test the offered high bay after stabilization at the declared electrical and thermal condition. If the product supports power selection, CCT selection or deep dimming, define which settings are covered.
For type approval, request whole-luminaire spectral or photometric data rather than relying only on the LED-package datasheet. The LM-79, LM-80 and TM-21 procurement guide explains why component and complete-product reports answer different questions.
6. Control production batches and later replacements
A type-test value does not guarantee that every shipment uses the same LED bin. Freeze the approved LED manufacturer, package, binning rule, board configuration, drive current and relevant optical materials. Require written approval before substitutions.
For each production lot, retain:
- LED reel or bin codes and incoming inspection records;
- luminaire assembly lot and production date;
- measured chromaticity data for the agreed sample;
- instrument identification and calibration status;
- acceptance result against the declared center and limit;
- traceability between cartons, luminaires and production records.
Plan replenishment before installation. Buy project spares from the same production lot where practical, store them under suitable conditions and identify their intended zones. A replacement ordered years later may meet the same catalog SDCM value but use a different center point or LED generation.
7. Request data that shows the distribution
A certificate saying “SDCM ≤3” is less useful than a table or chromaticity plot showing the actual measured samples. Request individual x,y or u′,v′ values, the declared center, the boundary used and sample identification.
Review whether:
- all samples fall inside the declared tolerance;
- results cluster consistently or sit against opposite edges;
- mixed wattages and optic variants were represented;
- the tested CCT matches the quotation;
- measurement conditions match the rated configuration;
- the report covers initial variation only or also includes maintenance data.
Averages can hide outliers. Ten luminaires can have an acceptable mean while two units at opposite sides of the tolerance look different when installed together. The acceptance rule should apply to individual sampled units, not only the batch average.
8. Build an incoming or pre-shipment inspection plan
Visual comparison helps detect a severe mismatch, but it is not a controlled measurement. Surroundings, adaptation, wall color and instrument exposure can change perception. Use a calibrated spectroradiometer or suitable measurement system under documented conditions for contractual acceptance.
- select samples randomly across cartons, production times and variants;
- stabilize luminaires under the agreed input and ambient condition;
- record individual chromaticity, CCT and Duv where specified;
- compare every result with the approved target and SDCM boundary;
- link failed units to LED-bin and assembly-lot records;
- define containment and re-inspection before shipment release.
Do not use a phone camera as the acceptance instrument. Automatic white balance can hide or exaggerate differences. Photos are useful for documenting the setup, not replacing spectral measurements.
9. Avoid five common supplier-comparison mistakes
Comparing only the nominal CCT
“4000K” alone does not define a single white point or batch spread.
Treating LED-package binning as whole-luminaire proof
The complete thermal, electrical and optical system must be represented.
Mixing different target centers
Two products can each meet 3 SDCM around different centers and still mismatch.
Checking only the average
Outliers matter because adjacent units are viewed individually.
Ignoring spares and phased orders
Initial uniformity can be lost when replacement stock comes from an uncontrolled later batch.
LED high-bay SDCM RFQ wording
Use project-specific values in the brackets:
The complete LED high-bay luminaire shall have initial color consistency of no more than [3/5] SDCM around the supplier-declared target chromaticity for [nominal CCT]. The supplier shall state the target coordinates, coordinate system, SDCM boundary, Duv target or range, rated input, stabilization condition and measurement uncertainty. Submit whole-luminaire test data for the offered model and production-lot chromaticity results for the agreed sample. LED package, binning rule, board, drive current and optical-material substitutions require written approval. Supply [quantity/percentage] project spares from the same controlled production lot where practical.
Add color-maintenance criteria separately if long-term chromaticity shift matters. Add CRI or TM-30 criteria separately if the visual task involves color discrimination. One line cannot substitute for all three requirements.
Final purchasing checklist
Before approving a 3-SDCM or 5-SDCM high-bay offer, confirm that:
- the tolerance matches the visual and replacement risk of each zone;
- target chromaticity and measurement conditions are declared;
- evidence applies to the complete offered luminaire;
- individual samples—not only averages—must pass;
- production binning and component changes are controlled;
- lot records and inspection data remain traceable;
- project spares and future replacements have a color-matching plan.
The best specification is not automatically the smallest SDCM number. It is the tightest tolerance the project genuinely needs, supported by measurable whole-luminaire evidence and a production plan that preserves the result.